
 English
 中文简体

How to Match an Automatic Canning Machine to Your Metal Packing Materials
Sep 11, 2026
At 9:00 a.m. on a typical production day, a canning line running at 380 cans per minute stopped because the two-piece can body steel suddenly deviated by 0.02 mm in thickness. The automatic canning machine was not the piece that broke. The material was outside the machine's clamping tolerance. The result was a 40-minute downtime and 1,900 rejected shells before the operator reset the parameters.
The conclusion is simple: an automatic canning machine only performs as well as the material and process alignment around it. If you are evaluating a machine, your first task is not to compare speed numbers. Your first task is to define how your metal stock, coating, and tolerances will interact with that machine.
Content
- 1 What automatic canning machine performance really depends on
- 2 Material tolerance: the silent driver of automatic canning machine efficiency
- 3 Choosing an automatic canning machine for your product mix
- 4 Changeover and maintenance: where hidden costs appear
- 5 A straightforward way to evaluate automatic canning machine investments
What automatic canning machine performance really depends on
An automatic canning machine in a metal packaging environment handles three main functions: forming, joining, and sealing. For three-piece cans, the machine feeds a rolled sheet or a coil of can body steel, forms the body, welds the side seam, and flanges both ends. For two-piece cans, the machine draws a cup from a coated coil and then presses it to shape. The machine's feed system, tooling, and sensors are designed around dimensional specifications.
That means the actual output depends on how precisely your material matches the machine's design window. If the steel coil is too hard, the forming rolls may slip. If the coating is too thick, the weld temperature needs adjustment. If the surface has a specific print registration, the machine's vision system must be able to see it consistently.
On a three-piece line, the material is usually a coated sheet or coil that is cut to length. The automatic canning machine then forms the body cylinder and welds the seam. The weld is the most sensitive part. A minor variation in the tin coating thickness can change the welding current requirement by 3-5 percent, which forces the operator to adjust the machine. If the adjustment is repeated many times per shift, the machine's total effective output drops faster than the nameplate rating suggests.
In practice, most packaging manufacturers see these issues much later than they expect. A line that was running a single-color can body steel may seem fine until you switch to a multicolor printed coil. The automatic canning machine's position sensors detect a darker or lighter substrate as a different reference point, and every subsequent operation shifts. This is where the choice of can body steel becomes a machine selection issue, not just a purchasing issue.
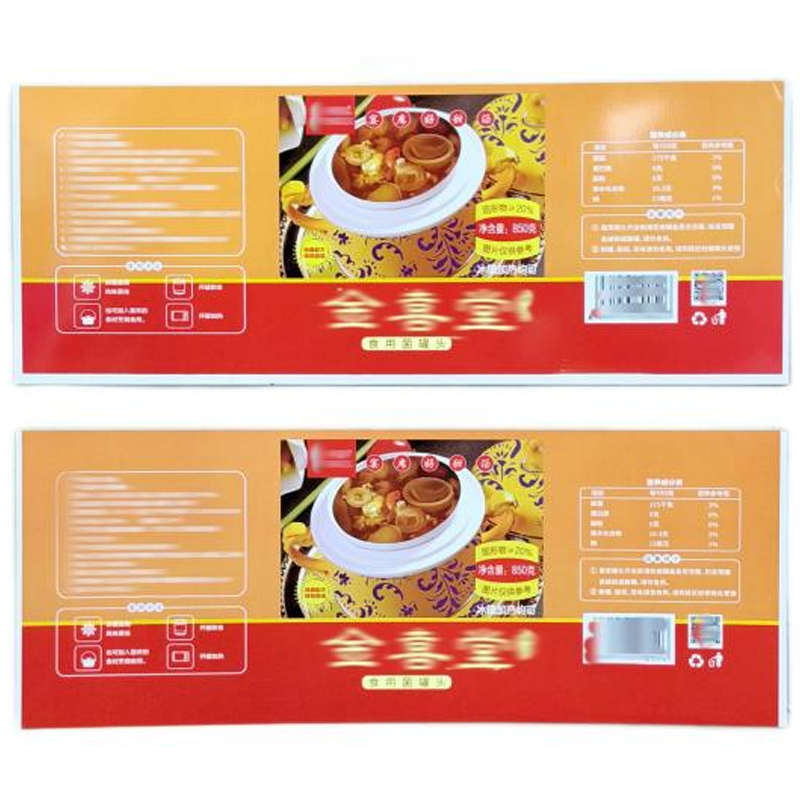 Multi-color printed three-piece can body steel for packagingThis tinplate or laminated steel offers multi-color printing with tin coating from 1.1 to 11.2 g/m² and thickness tolerance of ±0.01 mm. Its consistent surface helps prevent sensor misalignment in automatic canning lines.View Product →
We will expand on the tolerance dimension below.
Material tolerance: the silent driver of automatic canning machine efficiency
When you compare automatic canning machines, the literature often highlights cycle time and changeover features. However, the most costly failures are usually caused by material tolerance drift. For example, if a supplier delivers a tinplate coil at 0.29 mm instead of the specified 0.28 mm, the body-forming station may still handle it. But when the thickness varies along the same coil, the welding current becomes unstable. The machine begins producing weak seams, and the quality control team cannot isolate whether the issue is the machine, the coil, or the operator.
The table below shows typical tolerance expectations for materials used on a modern automatic canning machine.
| Material parameter | Typical working window | Impact when exceeded |
|---|---|---|
| Thickness | 0.18-0.30 mm | Feed jams and inconsistent welds |
| Coating weight | 2.8-5.6 g/m2 | Poor corrosion resistance or flaking |
| Hardness | 52-62 HRC | Springback and misshapen can bodies |
Coating weight is another variable that affects sealing and side-seam welding. For a food product with a short shelf life, a 2.8 g/m2 coating may be acceptable. For an aggressive food product like tomatoes, the iron dissolution rate becomes a concern. An automatic canning machine that is set up for one coating weight will not automatically adapt to another without a changeover. This is a common source of hidden downtime.
For the lid, the same principle applies. An EOE stock that is cut with a slight burr may not affect a slow manual line, but an automatic canning machine at 600 cans per minute will detect that burr as a feeding fault. The result is a false jam or a damaged lid. That is why selecting a reliable EOE material matters as much as selecting the machine brand.
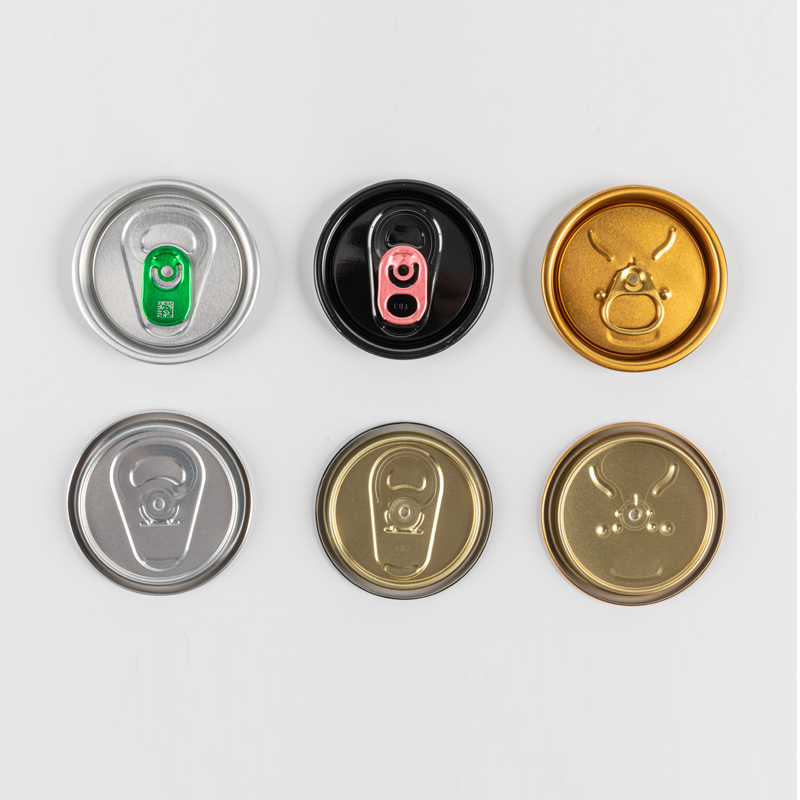 Beverage EOE stock with customizable coating and end typesSuitable for juice and beer, this EOE stock supports multiple end types and customization options. A clean cut reduces false jams and damaged lids in high-speed canning operations.View Product →
When you specify tolerances, you reduce the risk of these small but expensive interruptions.
Choosing an automatic canning machine for your product mix
Your product mix determines which machine features actually matter. A plant that produces only two-piece beverage cans has a different requirement from a plant that makes many small runs of three-piece food cans.
- Two-piece lines: high speed, low material consumption, but limited body shape flexibility.
- Three-piece lines: can run different diameters and heights, but side-seam welding needs precise material and coating.
- Multicolor printed bodies: require the automatic canning machine's registration system to be compatible with the printed repeat length.
Because the print and coating layers are applied before the can is formed, the machine's performance depends on the quality of that coating. A uniform coating produced on a coil coating line reduces friction variation and improves weld consistency.
Beyond material, the equipment itself needs to match your intended line speed and future expansion. A light-duty machine may handle 150 cans per minute, while a heavy-gauge line can exceed 800. The decision should be based on your actual annual volume, not on the machine's maximum theoretical speed.
Speed is not a neutral parameter. When you increase the line speed above 500 cans per minute, the sheet feeding becomes more dynamic. The belt tension, the vacuum cups, and the forming presses all have to operate at a faster rhythm. If your can body steel has a uniform hardness and a stable coating, that high speed is possible. If the material has slight variations, the machine will either produce more rejects or you will have to slow it down to maintain quality. Therefore, the actual speed you get is limited by the quality of your input material.
 Equipment support for canning line stabilityThis equipment company provides machinery and industry knowledge. With uniform input materials, their systems maintain performance at higher speeds, reducing rejects and ensuring predictable operation.View Product →
When you combine the right coating, the right can body steel, and the right equipment, you get a system that runs predictably.
Changeover is the second largest source of lost output after breakdowns. On an automatic canning machine, changeover includes replacing the forming tools, resetting the seam welding parameters, and loading a new coil. If your line runs multiple product sizes, you need to estimate how many minutes each change takes.
- Remove and clean the former dies; total time can exceed 20 minutes on older machines.
- Retune the welder for the new steel thickness; an experienced operator needs 10-15 minutes.
- Feed and register the new coil; this can take another 5 minutes.
These times become budget items. A machine with quick-change tooling may cost 15 percent more upfront but save more than that in labor over a year. The same logic applies to quality checks. A strict quality control process in your incoming material inspection prevents many of these changeover surprises.
Maintenance is not simply about lubrication or belt replacement. An automatic canning machine that runs with a misaligned former will gradually wear the dies. That wear shows up as dimensional drift in the cans, and the quality team will notice an increasing number of cans that fail the micrometer check. If you have a robust material inspection process, you can always distinguish between die wear and incoming material variation. Without it, the maintenance team may replace perfectly good tooling.
A straightforward way to evaluate automatic canning machine investments
The evaluation of an automatic canning machine should start with your material specification, not with the machine brochure. Write down the actual thickness range, coating weight, and surface finish for every product you plan to run. Then ask the equipment supplier to prove that the machine's feeding, forming, and sensing systems can handle your existing inbound coil tolerance.
When you invite an equipment supplier, ask them to bring a sample of your material or ask them to run a trial on their own machine. The trial should include three cases: your average material, your tightest tolerance, and the worst-case coil you receive from your current supplier. If the machine can produce acceptable cans in all three cases, it has a real operating margin. If it can only handle the average material, you are buying a machine that will fail during normal production fluctuations.
An automatic canning machine is only as stable as the weakest input in the line. If your supplier can demonstrate stable performance with your current materials, you have found a reliable partner. If they can only demonstrate performance with their own reference material, you are absorbing a technical risk that will appear in your production report later.
Start with what you are actually processing, and the machine decision becomes much easier.

- Address: No. 11 Zhenxing Road, Hangzhou Bay Shangyu Economic and Technological Development Area, Zhejiang, China
- Phone: +86-137 5814 2106 / +86-130 1771 8906
- TEL: +86-575-8272 2388 / +86-575-8272 2366
- E-mail: sales@hz-jinma.com

 sales@hz-jinma.com

